Choosing a reliable Mcb Inspection Conveyor manufacturer in China requires more than comparing prices. The right supplier should understand miniature circuit breaker production, electrical testing, indexing accuracy, and long-term equipment stability. A well-designed conveyor can move each MCB smoothly between assembly, inspection, marking, and packaging stations. It should also reduce manual handling without hiding quality problems.
Ethan Zhang, an industrial automation engineer specializing in circuit breaker lines, states, “An MCB Inspection Conveyor is valuable only when it makes defects visible and production decisions measurable.” His view reflects a practical issue. Speed alone does not create a dependable inspection system. Sensors must detect missing parts, incorrect positions, damaged housings, and inconsistent terminal placement. The conveyor frame should remain stable during repeated starts and stops. Even a small vibration can affect camera focus or electrical testing accuracy.
Experienced Chinese manufacturers usually provide customized layouts, PLC control, servo indexing, vision inspection integration, and after-sales support. They should also explain inspection tolerances clearly. Ask for sample testing, factory videos, reference projects, and maintenance instructions. These details reveal more than a polished website.
However, no conveyor suits every factory. Product dimensions, cycle time, testing voltage, floor space, and data requirements can change the design completely. A supplier may promise excellent performance, yet actual results depend on commissioning and operator training. That is where buyers must remain careful. The best evaluation combines technical documents, witnessed testing, and honest discussion about limitations. A China-based manufacturer becomes a strong choice when it delivers consistent accuracy, transparent communication, and a system that can be maintained years after installation.
MCB Inspection Conveyors: Definition and Core Functions
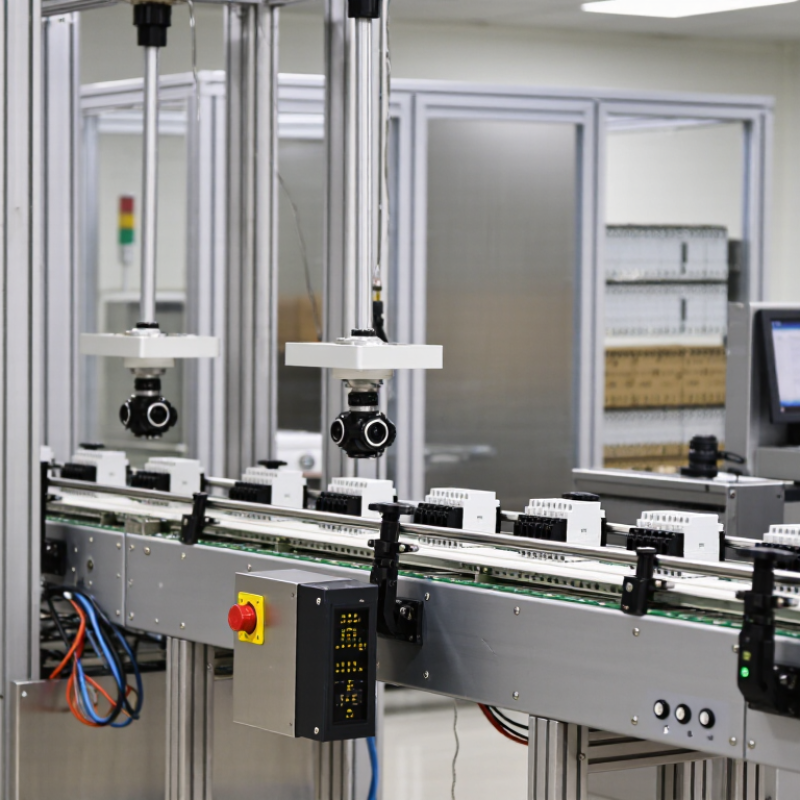
An MCB inspection conveyor is a controlled transport system for miniature circuit breakers. It moves each unit through visual, dimensional, electrical, and marking checks. Unlike a general belt conveyor, it manages pitch, orientation, and inspection timing. Servo indexing can pause products beneath cameras, while guides keep terminals aligned. A practical system also separates accepted and rejected units without stopping the main flow.
The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. This figure shows the wider shift toward automated handling and repeatable inspection. In MCB production, conveyors connect assembly, testing, labeling, and packing stations. Sensors can detect missing toggles, incorrect housings, surface damage, or unreadable codes. Data collection adds traceability, especially when each carrier receives a production timestamp.
A perfect line is a useful myth. Dust, vibration, and loose components still affect camera accuracy. Engineers should verify lighting, conveyor speed, and reject timing on the real product. The IEC 60898-1 standard defines important requirements for circuit breakers used in household and similar installations, but it does not design the conveyor itself. That distinction matters. Reliable inspection depends on both compliant products and carefully validated equipment. Small spacing errors can become large counting errors. 马会
MCB inspection conveyors transfer miniature circuit breakers through sequential inspection stations, including visual checks, dimensional verification, terminal inspection, continuity testing, dielectric testing, and trip-characteristic testing. The chart shows the instantaneous magnetic trip-current bands specified for common B, C, and D characteristics in IEC 60898-1, expressed as multiples of the rated current (In).
How to read the chart: A B-curve MCB should trip magnetically between 3 and 5 times In, a C-curve device between 5 and 10 times In, and a D-curve device between 10 and 20 times In. An inspection conveyor can route each product through the appropriate electrical test range based on its marked trip characteristic.
An MCB inspection conveyor begins with controlled loading. Operators place miniature circuit breakers into dedicated fixtures. Each fixture keeps the device upright and evenly spaced. The belt moves slowly. This prevents contact between neighboring units and protects sensitive parts during transfer.
As the conveyor advances, sensors confirm each fixture’s position. A camera checks the housing, terminal openings, label area, and switching lever. Some systems use lighting from several angles to reveal cracks, scratches, or incorrect assembly. A measuring station can verify height, width, and terminal alignment. The control unit compares each image with approved inspection settings. If a defect appears, an air nozzle or mechanical diverter separates the item from the accepted flow. Data is stored for traceability, including time, station, and defect type.
Inspection accuracy depends on stable speed, clean lenses, and properly adjusted fixtures. Small dust particles can create false alarms. That detail is often underestimated. Experienced technicians check sample units during every shift and review unusual rejection patterns. Conveyor calibration also requires regular attention, especially after maintenance or format changes. No line is perfect. A sensor may respond late, or a fixture may loosen slightly. Recording these events helps engineers improve the process instead of hiding its weak points. Reliable equipment should support careful human judgment, not replace it.
China Top MCB Inspection Conveyor Manufacturer?
Key Technologies Used in MCB Inspection Systems
A reliable MCB inspection conveyor combines mechanical control, machine vision, and electrical testing. The conveyor must position each breaker accurately. Small shifts can affect image results. Servo-driven indexing systems usually provide stable spacing and repeatable movement. Sensors confirm product presence before inspection begins. Vision cameras then check housing dimensions, terminal position, marking quality, and assembly details. Controlled LED lighting is essential. It reduces shadows around narrow terminal areas.
Electrical testing adds another layer of protection. Automated stations can verify continuity, insulation performance, and trip characteristics under controlled conditions. Test fixtures need firm contact without damaging terminals. A PLC coordinates conveyor movement, inspection timing, and reject signals. Safety interlocks should stop the system when guards open or testing becomes abnormal. This is practical engineering, not decoration.
Inspection data should connect each result with a serial number or production batch. Operators can then trace repeated defects and adjust upstream processes. However, vision systems are not perfect. Reflective plastic, dust, and uneven printing can create false alarms. Regular lens cleaning and fixture checks remain necessary. In some factories, inspection sensitivity is set too high, causing unnecessary rejection. That wastes time. Experienced technicians normally review sample images and test records before changing thresholds. A robust system also stores failed images, alarm histories, and calibration records for later analysis.
Choosing a Chinese MCB inspection conveyor manufacturer requires more than comparing prices. The system should handle stable indexing, terminal inspection, label reading, and controlled rejection.
The International Federation of Robotics reported 276,288 industrial robots installed in China during 2023, representing about 51% of global installations. This indicates strong automation capability, but robot density does not prove conveyor quality.
Ask for factory acceptance test records, cycle-time data, and sample inspection images. A reliable supplier should explain how sensors detect missing terminals, incorrect assembly, and surface damage. The conveyor must also support safe electrical integration under IEC 60898-1 requirements for miniature circuit-breakers. Request wiring diagrams, risk assessments, and component traceability. ISO 9001 certification helps, but it does not replace process evidence.
Look closely at the machine itself. Check belt alignment, fixture changeover, guarding, emergency stops, and noise near the operator station. A 2024 conveyor-system market report estimates the sector may grow from about 10.3 billion US dollars in 2023 to 13.2 billion by 2028. That growth encourages fast sales claims. Be careful. A polished video is not proof.
I would run mixed-size samples for several hours and record missed inspections, jams, and recovery time. One practical weakness often appears here: suppliers may demonstrate a perfect cycle, yet provide limited data for abnormal conditions. Ask how the system behaves after a sensor failure, product shortage, or sudden restart.
China Top MCB Inspection Conveyor Manufacturer?
A reliable MCB inspection conveyor supports production from molding to final packing. It can position breakers, check housing dimensions, inspect terminal screws, and identify missing labels. Camera stations need stable lighting, not only high resolution. Small shadows can hide cracks around terminal openings. Global electricity demand is forecast to grow by about 4% annually through 2025, according to the IEA Electricity 2024 report. That pressure encourages higher output, but speed must not weaken inspection accuracy.
Quality requirements should follow IEC 60898-1 for household and similar circuit breakers. The conveyor should also support ISO 9001 procedures, including calibration records, defect samples, and traceable inspection results. In practical commissioning, engineers should compare automated results with manual measurements. This step is often skipped. It should not be. A reject gate must separate defective units without damaging nearby products. Barcode or QR tracking can connect each MCB with test time, station number, and operator access records.
Customization depends on product size, pole configuration, and factory layout. Options may include adjustable guides, servo indexing, electrical test modules, vision cameras, and dust-resistant enclosures. Some lines need ESD control or controlled feeding from an assembly machine. Others require a compact U-shaped layout. A useful supplier should provide cycle-time validation using real samples, not only simulations. Even then, false rejects may appear after installation. That risk deserves review during acceptance testing, especially when product colors or screw finishes change.
| Data Dimension | Typical Specification or Requirement | Application in MCB Inspection Conveyors | Quality and Verification Considerations | Customization Options |
|---|---|---|---|---|
| Product Compatibility | Miniature circuit breakers, commonly one-pole, two-pole, three-pole, and four-pole configurations. | Transfers molded-case products between assembly, inspection, testing, marking, and packing stations. | Product nests and guides should match the MCB housing dimensions and terminal arrangement. | Adjustable guides, interchangeable nests, quick-change tooling, and multi-pole product fixtures. |
| Conveyor Type | Servo-driven indexing conveyor, belt conveyor, chain conveyor, or palletized transfer system. | Provides controlled movement and repeatable positioning for camera inspection and electrical testing. | Indexing accuracy, smooth motion, low vibration, and stable product positioning should be verified during commissioning. | Continuous or intermittent motion, customized transfer length, parallel lanes, and automatic buffering. |
| Typical Line Speed | Approximately 20–60 products per minute, depending on inspection steps and product design. | Supports medium- and high-volume MCB assembly lines. | Actual output depends on test duration, reject handling, changeover time, and the number of inspection stations. | Variable-speed drives, synchronized stations, additional lanes, and accumulation sections. |
| Visual Inspection | Camera-based or sensor-based inspection of housing, actuator position, labels, screws, terminals, and assembly presence. | Detects missing, misplaced, damaged, incorrectly assembled, or incorrectly marked components. | Lighting, camera resolution, inspection repeatability, and validated good/bad sample testing are important. | Top, side, bottom, or multi-angle cameras; barcode or QR-code reading; customized lighting and software rules. |
| Electrical Testing | Common tests may include continuity, insulation resistance, dielectric withstand, and trip-function verification. | Confirms electrical performance after mechanical assembly and before final packing. | Test voltage, current, duration, insulation resistance, and acceptance limits must follow the approved product specification and applicable standards. | Integrated test modules, automatic contact probing, programmable test recipes, data logging, and reject isolation. |
| Applicable Product Standards | IEC 60898-1 is commonly relevant to circuit-breakers for household and similar installations; IEC 60947-2 applies to circuit-breakers within low-voltage switchgear and controlgear requirements. | Provides a reference framework for product testing, inspection planning, and acceptance criteria. | The applicable standard depends on the MCB product category, rated values, intended use, and market requirements. | Inspection recipes can be configured for different ratings, pole counts, tripping characteristics, and customer specifications. |
| Machinery Safety | Risk assessment, guarding, emergency stops, safe access, and appropriate electrical control protection should be included. | Protects operators around moving conveyors, pneumatic mechanisms, electrical probes, and automated reject devices. | Design should be reviewed against applicable machinery, electrical safety, and workplace safety requirements in the target market. | Safety doors, light curtains, interlocked guards, safety relays, warning indicators, and customized access layouts. |
| Control System | PLC-controlled operation with a human-machine interface for status display, recipe selection, alarms, and parameter adjustment. | Coordinates conveyor movement, inspection triggers, testing sequences, and reject actions. | Control logic should include fault detection, sensor diagnostics, password management, and controlled restart procedures. | Multilingual interface, production dashboards, remote diagnostics, line integration, and manufacturing data connectivity. |
| Traceability | Recording of product code, serial or batch number, inspection result, test value, date, and station information. | Supports quality analysis, process monitoring, and targeted product recall when required. | Data integrity, timestamp accuracy, access control, backup, and retention periods should be defined before acceptance. | Barcode scanners, QR-code readers, database export, network connection, and integration with MES or ERP systems. |
| Reject Handling | Automatic separation of failed products into a controlled reject bin or locked reject area. | Prevents nonconforming MCBs from continuing to packing or shipment. | Reject confirmation, bin-full detection, fault alarms, and manual reinspection procedures should be provided. | Pneumatic pushers, servo diverters, separate reject lanes, lockable containers, and reject reason classification. |
| Changeover | Manual or assisted adjustment for different MCB sizes, pole configurations, or product families. | Allows one inspection line to process multiple product variants. | Changeover time, repeatability, tool identification, and first-piece approval should be documented. | Digital position indicators, recipe-controlled settings, tool detection, quick clamps, and modular fixtures. |
| Conveyor Materials | Common construction uses coated carbon steel or stainless steel for frames, with engineering plastics or wear-resistant materials for product-contact parts. | Provides mechanical support and stable product transfer in production environments. | Material selection should consider corrosion, cleaning method, dust, temperature, electrical insulation, and product-contact requirements. | Stainless-steel frame, cleanroom-compatible components, antistatic parts, corrosion-resistant fasteners, and special surface finishes. |
| Pneumatic Requirements | Where pneumatic actuators are used, clean and regulated compressed air is generally required; actual pressure depends on the selected components. | Operates product clamps, stoppers, pushers, lifters, and reject mechanisms. | Air filtration, pressure monitoring, leakage control, drainage, and safe loss-of-pressure behavior should be evaluated. | Low-noise valves, pressure sensors, vacuum handling, compact cylinders, and pneumatic consumption monitoring. |
| Acceptance Testing | Factory acceptance testing and site acceptance testing should cover throughput, inspection accuracy, safety functions, changeover, and data records. | Confirms that the completed conveyor meets the agreed functional requirements before production release. | Use approved test plans, reference samples, capability checks, alarm verification, and documented punch-list closure. | Customer-defined acceptance criteria, sample quantities, performance reports, operator training, and validation documentation. |
| Maintenance | Routine cleaning, sensor alignment checks, belt or chain inspection, lubrication where applicable, and electrical safety checks. | Helps maintain stable positioning, inspection accuracy, and equipment availability. | Maintenance intervals should be based on operating hours, environment, component recommendations, and production experience. | Condition monitoring, preventive-maintenance reminders, spare-parts kits, remote support, and maintenance access panels. |
| Documentation | Typical documentation includes user manuals, electrical drawings, pneumatic diagrams, parts lists, software backups, and maintenance instructions. | Supports installation, troubleshooting, operator training, and future line modifications. | Documents should match the delivered equipment and include revision control. | Customized documentation language, digital document packages, validation records, and customer-specific formats. |
| Customization Scope | Layout, product range, inspection sequence, line speed, control interface, data system, and safety architecture can be engineered around the production process. | Enables integration with upstream assembly equipment and downstream packaging or palletizing systems. | Customization should begin with product drawings, cycle-time data, inspection criteria, utility conditions, and factory layout constraints. | Turnkey line integration, compact layouts, multi-lane systems, robotic loading, custom testing, and automated packaging transfer. |
| Supplier Evaluation Criteria | Relevant experience, technical design capability, inspection repeatability, service response, documentation quality, and commissioning support. | Helps buyers compare inspection conveyor solutions beyond purchase price alone. | Request representative test results, acceptance procedures, reference samples, warranty terms, and spare-parts arrangements. | Technical workshops, feasibility testing, pilot units, staged implementation, and service agreements. |
| Important Note | The specifications shown are typical planning references rather than universal requirements. Final conveyor dimensions, speed, inspection methods, electrical test parameters, safety design, and applicable standards should be confirmed through the product drawings, risk assessment, approved technical specification, and target-market regulations. | |||
1901 West Main Street
Washington, MO 63090
Main Directory: 1-800-227-4873
Email: sale@pangcofurniture.com

We’re always looking for talented individuals to join our team. Send us your resume using the form below. When a position comes available that matches your skillset, one of our team members will reach out to you.
"*" indicates required fields