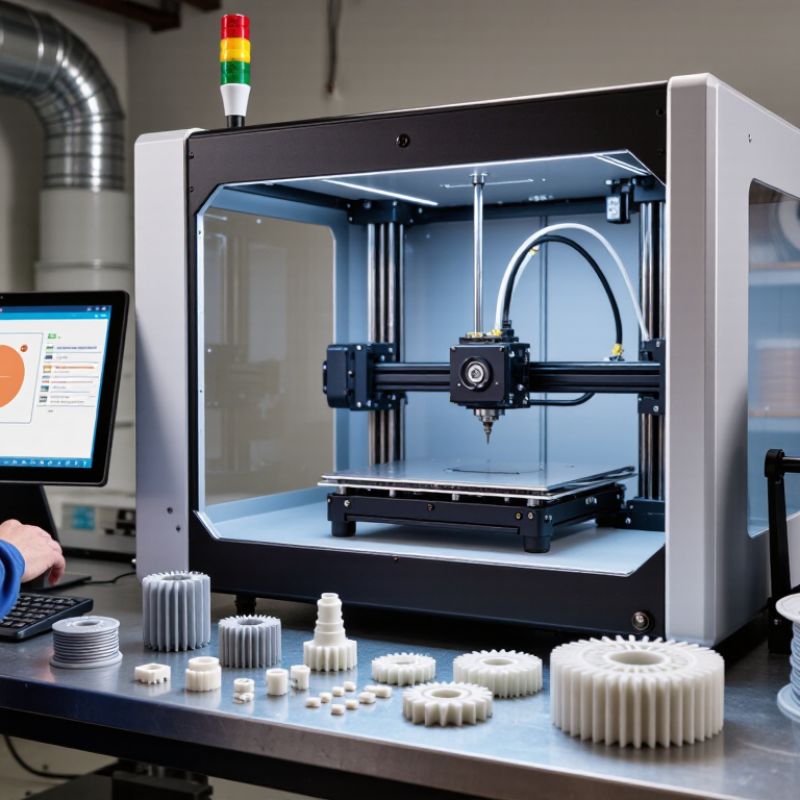
| Fused Filament Fabrication (FFF/FDM) | PA6, PA66, PA12, and glass- or carbon-fiber-reinforced nylon filaments | Desktop, professional, or industrial material-extrusion printer with a heated chamber preferred | Approximately 200 × 200 × 200 mm to 1,000 × 1,000 × 1,000 mm | Typically ±0.10–0.30 mm, depending on machine size, calibration, and part geometry | Low to medium; generally suitable for one-off parts and small batches | Often required for overhangs and complex geometries; soluble supports may be available on dual-extrusion systems | Approximately US$2,000–US$250,000, excluding accessories and post-processing equipment | Nylon filament is hygroscopic and should be dried and stored in a sealed, low-humidity container. Warping can be reduced with a heated bed, enclosure, and controlled chamber temperature. | Functional prototypes, fixtures, jigs, tooling, replacement parts, and customized low-volume components | Good for flexible production |
| Selective Laser Sintering (SLS) | PA12, PA11, and selected reinforced polyamide powders | Industrial powder-bed fusion system with powder handling and controlled thermal conditions | Approximately 250 × 250 × 300 mm to 400 × 400 × 400 mm | Typically ±0.10–0.30 mm, with shrinkage and thermal behavior considered during design | Medium to high for nested batches; multiple parts can be produced in one build | Not normally required because unsintered powder supports the parts | Approximately US$50,000–US$250,000, plus powder-processing and finishing equipment | Powder must be sieved, stored properly, and managed according to the machine’s refresh and reuse requirements. Parts usually need depowdering and bead blasting or another finishing process. | End-use parts, enclosures, ducts, housings, complex assemblies, and customized production batches | Very good for complex parts |
| Multi Jet Fusion (MJF) | Primarily PA12 and PA11 powders, with selected reinforced polyamide options | Industrial powder-bed fusion production system with automated powder handling | Approximately 300 × 300 × 300 mm to 400 × 400 × 400 mm | Typically around ±0.10–0.30 mm, depending on part size, orientation, and process calibration | High for repeatable batch production and densely packed builds | Not normally required because surrounding powder supports the parts | Approximately US$100,000–US$500,000, with additional costs for powder management and finishing | Requires a controlled production area, reliable powder workflow, and post-processing capacity. Thermal uniformity and packing density strongly influence consistency. | Series production, spare parts, consumer products, medical housings, and lightweight functional assemblies | Excellent for batch manufacturing |
| High-Temperature FFF/FDM | PA6, PA66, PEKK-based polyamides, and fiber-reinforced high-performance nylon blends | Industrial printer with a high-temperature nozzle, heated build chamber, and heated build platform | Approximately 300 × 300 × 300 mm to 1,000 × 1,000 × 1,000 mm | Typically ±0.15–0.40 mm, influenced by thermal shrinkage and reinforcement content | Low to medium; optimized for large, strong parts rather than maximum output speed | Usually required for complex overhangs; support removal can be difficult with reinforced materials | Approximately US$50,000–US$300,000, depending on chamber temperature and automation level | Requires strict control of filament moisture, chamber temperature, nozzle wear, and thermal gradients. Abrasive fiber-filled filaments may require hardened nozzles. | Automotive tooling, aerospace fixtures, industrial equipment parts, and high-temperature functional prototypes | Excellent for demanding applications |
| Low-Cost Desktop FFF/FDM | Basic PA12 or nylon blends, usually with limited fiber reinforcement | Entry-level or prosumer enclosed printer with a heated bed and filament dryer | Approximately 180 × 180 × 180 mm to 300 × 300 × 300 mm | Typically ±0.20–0.50 mm, depending on setup and operator skill | Low; best suited to prototypes and occasional parts | Frequently required for complex shapes | Approximately US$500–US$5,000, excluding dryers, hardened nozzles, and spare parts | Results can vary significantly with moisture control, bed adhesion, cooling, and printer enclosure quality. It is less suitable for unattended production. | Design validation, educational use, maintenance parts, simple fixtures, and early-stage product development | Best for low-budget entry |
| Nylon Composite FFF/FDM | Nylon reinforced with short carbon fiber or glass fiber | Professional or industrial extrusion printer with a hardened nozzle and strong heated platform | Approximately 200 × 200 × 200 mm to 600 × 600 × 600 mm | Typically ±0.15–0.35 mm; fiber reinforcement can reduce warping but may increase anisotropy | Low to medium | Often required, especially for large overhangs and vertically oriented features | Approximately US$5,000–US$150,000 | Fiber-filled nylon offers higher stiffness and better dimensional stability, but it can be more abrasive and less impact-resistant than unfilled nylon. | Lightweight brackets, robotic tooling, fixtures, drone components, and structural prototypes | Very good for stiff tooling |