Ball end mills shape curved surfaces, deep cavities, and detailed contours that flat cutters cannot reach cleanly. Their rounded tips leave smooth transitions, but tool choice changes cutting forces, reach, finish, and tool life. Small details matter.
Manufacturing engineering author Serope Kalpakjian is a respected voice in production technology. The following line is a practical paraphrase of manufacturing principles, not a verbatim quotation: “Choose cutting geometry to match the material, feature, and finish.” That rule helps organize this guide. It also keeps selection grounded in the workpiece, not marketing claims.
This overview compares common Ball End End Mill types, including standard, tapered, long-reach, and micro designs. It explains where each geometry performs well and where it may struggle. A tapered tool can reach angled walls; a long-reach tool accesses deep pockets, but added length can increase deflection. Micro tools capture fine details. They need careful handling.
Coatings, flute counts, and carbide grades also affect performance. Yet no single type suits every machine, material, or setup. Real results depend on rigidity, toolpath, and cutting conditions, so published guidance should be tested against the actual job. A useful starting point. The sections ahead connect each tool type with practical applications, selection trade-offs, and common limits. Expect clear comparisons, not a universal winner.
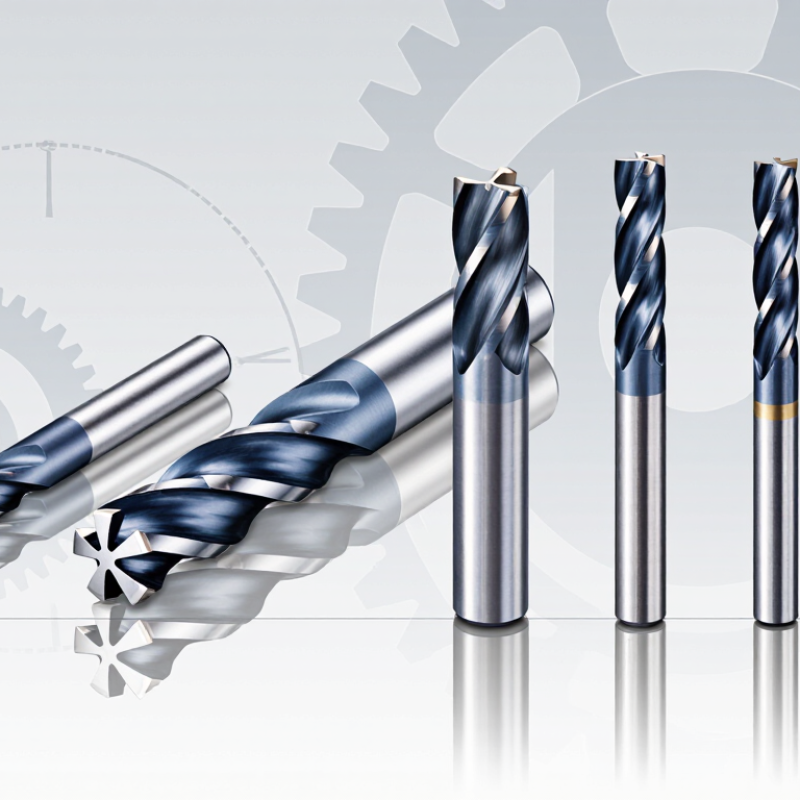
Ball end mills are commonly classified by the shape of their cutting ends and the work they perform. A standard ball nose cutter has a rounded tip and is widely used for curved surfaces, sculpted contours, and mold cavities. Its tip leaves a smooth, concave path, though the very center cuts slowly because its surface speed approaches zero. Toolpath planning matters.
Tapered ball nose mills combine a rounded tip with a narrowing, angled neck. This shape adds stiffness and helps reach deep, narrow features, such as fine channels in a mold. Small details matter. Micro ball end mills serve miniature parts and delicate features, but their small diameters can make them sensitive to runout and vibration. A rigid setup is essential.
Application also separates roughing and finishing choices. Larger ball mills can remove material from broad contours, while smaller tools reach tight radii and add detail. Finishing passes usually use light cuts and close stepover spacing to reduce visible scallops. The right choice depends on material, cavity depth, machine rigidity, and the desired surface. A chart helps, but a short test cut often exposes practical limits that geometry alone cannot predict.
Standard ball end mills have a rounded, hemispherical cutting tip that suits general contouring. The shape lets the tool follow curved walls, blended transitions, and shallow 3D profiles without leaving sharp internal corners. On a mold cavity, for example, it can trace a concave surface while keeping the cut continuous. That matters.
Tool diameter and corner radius affect access and finish. A smaller tool reaches tighter details, but its slender cutting end may deflect more under load. For broad contours, a larger diameter is often more rigid and can remove material faster. Not always. Material hardness, flute design, machine stiffness, and toolpath strategy all change the result, so avoid choosing by diameter alone.
The rounded tip does not cut like a flat end mill. Near the center, cutting speed is low, which can encourage rubbing if the toolpath pushes the tip directly into the work. A slight lead or tilt, where the setup allows it, can improve engagement. Stepover also leaves visible scallops on a sloped surface; reducing it usually smooths the finish but increases machining time. Check the finish. A practical test cut can reveal chatter, tool marks, or unexpected wear before a long contouring job begins. Even then, the best setting may need adjustment.
Standard ball end mills are commonly used for curved surfaces and 3D contours. The chart compares theoretical scallop height at several stepover widths for three cutter diameters. Smaller scallops generally produce a smoother surface.
Ideal geometric values in millimeters, calculated as h = R − √(R² − (s/2)²), where R is the ball radius and s is the stepover. Actual results vary with tool deflection, runout, material, and machining conditions.
Tapered ball end mills suit deep pockets, drafted walls, and angled transitions where a straight neck may rub the workpiece. Their wider upper section adds support behind the cutting head, while the narrow end reaches confined areas. The taper angle must still clear the wall, including tool runout and expected deflection. A small mismatch can leave a bright rub mark. Not ideal.
Consider a 3-degree taper over 25 millimeters: the diameter changes by about 2.6 millimeters. This geometry calculation helps estimate clearance, but it is not a cutting recommendation. At the ball’s exact center, cutting speed approaches zero, so toolpaths often tilt the cutter to move contact away from that point. ISO 8688-2:1989 provides a framework for milling tool-life tests using cutting time and defined failure criteria. That is useful when comparing wear, rather than judging a tool by reach alone. In practice, chip evacuation and holder clearance can still limit a deep cut. The neat geometry rarely tells the whole story.
Micro ball end mills are suited to fine contours, narrow slots, and small cavities that larger cutters cannot reach. Their rounded tips leave smooth transitions between floors and walls, especially on sculpted surfaces. A CIRP Annals review by Dornfeld, Min, and Takeuchi (2006) describes micromachining as producing features from 1 to 999 micrometers. That range explains why even tiny setup errors can show up clearly on a finished part.
Match the ball radius to the cavity’s smallest internal radius, and keep the tool’s stickout short to limit deflection. Runout matters. At micro scale, uneven tooth engagement can make one cutting edge do most of the work, causing rough patches or early wear. Use a stable spindle, suitable feed, and modest radial engagement; then inspect the actual cut, not just the simulation. Small details matter. A practical caution: the smallest tool is not always the best choice. If it bends or chips, a slightly larger radius may hold tolerance better, though it can leave corners less sharp.
Roughing ball end mills remove stock quickly while following curved or sculpted surfaces. Some use coarse or chip-breaking cutting edges to split long chips into smaller pieces. This can help clear chips from deep pockets and maintain steadier cutting. The rounded tip also follows contours that would leave sharp steps with a flat end mill.
But high removal rates are not automatic. Tool reach, flute geometry, material, and machine rigidity all matter.
A practical approach is to use a toolpath with consistent engagement and leave a small, even allowance for finishing. In a mold cavity, for example, check that chips escape rather than collecting around the tool. Listen for chatter and watch spindle load; both can signal that the cut is too aggressive.
It is tempting to chase the largest cut. That is not always productive. Roughing often leaves visible scallops, and a ball end mill with long reach may flex under heavy load. Reducing feed or radial engagement can improve stability, though it may slow stock removal. The best setup balances removal rate, tool life, and the finishing work still ahead.
1901 West Main Street
Washington, MO 63090
Main Directory: 1-800-227-4873
Email: sale@pangcofurniture.com

We’re always looking for talented individuals to join our team. Send us your resume using the form below. When a position comes available that matches your skillset, one of our team members will reach out to you.
"*" indicates required fields